Although aerospace bearings might be seemingly less glamorous than other parts—think engines and wing assemblies—their role is instrumental. Read on to learn more about aerospace bearings and what sets them apart.
What Are Aerospace Bearings?
Aerospace bearings are components that support moving parts in an aircraft while withstanding demanding operating conditions.
Compared with bearings used in other applications, aerospace bearings need to perform under extreme temperatures, high speeds, heavy loads, vibration and strict weight requirements. Depending on the application, they may also need to resist corrosion and operate with minimal lubrication or maintenance.
“Many of the critical components of aircraft engines and landing gear need to be able to move, and the goal of any bearing is to allow for two mated surfaces to rotate, either linked or independently of each other,” says Andrew Biro, advanced application engineering manager for abrasives manufacturer Norton Saint-Gobain.
Biro gives the example of a turbofan.
“The bearings need to withstand both the axial and centrifugal forces during operation,” he explains. “At the same time, they need to rotate efficiently—without excess friction, which can reduce life or damage the bearings.”
Types of Aerospace Bearings
Aircraft bearings are selected to suit the load, movement, space and operating conditions of each application.
Ball Bearings
These hardened balls between inner and outer races reduce friction and support rotational movement. Depending on design, they handle radial and axial loads, making them suitable for smooth, high-speed applications such as engines, gearboxes, accessories and flight controls.
Roller Bearings
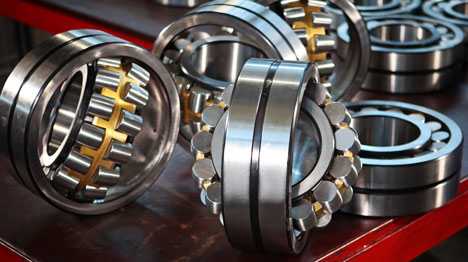
These use cylindrical, tapered or spherical rolling elements to carry high loads. Cylindrical designs handle primarily radial loads; tapered designs support combined radial and axial loads; and spherical designs accommodate heavy loads and some misalignment.
Plain and Spherical Plain Bearings
Plain bearings use sliding surfaces rather than rolling elements, often with a low-friction liner. Their compact design suits limited space and applications involving oscillating movement. Spherical plain bearings also allow angular motion and accommodate misalignment, including in control systems and landing gear.
Rod End Bearings
Rod end bearings combine a bearing with a threaded shank to connect components while allowing angular movement.
Where Are Bearings Used in an Aircraft?
Bearings are used throughout an aircraft to support movement and manage loads, vibration, temperature and contamination.
Engines
Engine bearings support shafts and other rotating components at high speeds and temperatures.
Landing Gear
Landing gear bearings guide components as the gear extends and retracts and help them withstand landing and taxiing loads. Plain, spherical plain and roller bearings may be used; durability and protection from moisture and contaminants are important.
Flight Control Systems
Bearings at hinges, pivots and linkages allow precise movement of control surfaces. Spherical plain bearings and rod ends are common where components move through small, repeated angles rather than rotating continuously.
Rotors and Gearboxes
Helicopter rotor hubs commonly use laminated elastomeric bearings to accommodate blade pitch, flap and lead-lag movement. Gearboxes use ball, roller or other specialized bearings to support shafts and gears as they transmit power.
What Makes Aerospace Bearings Different?
Aircraft contain bearings throughout their engines, landing gear and rotors, where they must withstand extreme operating conditions.
“If we look at regular landing gear on a winged aircraft, you’ve got bearings in tires, wheels, brakes, etc.,” says Kevin Giardiniere, regional product manager for turning–PCBN, ceramics at Kennametal. “These have to survive in a wide range of temperatures—moving from 30 or 40 degrees below zero at cruising altitude to impact, where they quickly reach their highest temperature while moving at high speed.”
As aircraft become lighter, faster and more fuel-efficient, engine operating temperatures continue to rise. “We’re talking bearings rated to operate close to 900 or more degrees Fahrenheit on a continual basis,” he says.
Aerospace bearings must also resist corrosion from exposure to saltwater and salt air, as well as wind, rain, dust, heat and cold.
The Evolution of Aerospace Bearing Materials
Given the extreme demands placed on these assemblies, bearing materials have become highly specialized.
“Today’s aerospace materials have evolved to provide longer life, operation at an ever-higher temperature range and better corrosion resistance,” Giardiniere says.
These factors, along with the need to minimize maintenance, reduce weight and conserve fuel, are the drivers behind the changes and improvements.
Materials Used in Aerospace Bearings
Each of these materials is selected based on the distinct characteristics of the metals and the environments where the assemblies will be used—in landing gear versus an engine, for example.
• Alloy 52100 steel is the most popular material by volume used in the bearing industry. It’s a through-hardening-type material with the same hardness from the surface into the core and then out through the other side.
• M50 tool steel is a variant in the same family as 52100, but even though it’s through-hardened, it can operate in a higher temperature range than 52100.
• M50 NiL (a low-carbon, high-nickel variant of M50) has been modified with the addition of nitrogen, which allows it to be case hardened on the outside while maintaining a softer core material. That makes the outer surfaces wear-resistant but leaves the inner core somewhat flexible, allowing it to adhere a bit and expand with a hot shaft, in order to prevent cracking.
• 440C stainless steel is highly resistant to corrosion, making it a common material for an exposed bearing that will see weather and possible immersion in saltwater, as well as exposure to hot and cold thermal cycling and interaction with oxygen.
• SiN is a ceramic material commonly used for high-speed ball bearings. It is highly wear-resistant, so the bearings can last quite a bit longer than a traditional heat-treated steel bearing.
• HRSAs, or heat-resistant superalloys, are used in aerospace bearings for their corrosion resistance and retention of strength and hardness at high temperatures. Nickel-based HRSAs, such as Inconel 718, are the most widely used and constitute more than 50 percent of the weight of advanced aircraft engines. Cobalt-based HRSAs are even more corrosion-resistant at high temperatures and are used for combustion parts in the hottest engine areas.
How Aerospace Bearings Are Manufactured
“The need to meet these exacting requirements with such high reliability drives all aspects of bearing manufacturing to be as perfect as possible—from specialized materials to the processes used to create them,” Giardiniere says.
Manufacturing a precision bearing for aerospace starts with an initial roughing operation with a strong carbide tool. Next, a bearing is sent for a heat-treating process to be either through-hardened or case-hardened. A machinist then works the surfaces close to a final shape, before either hard turning or finish grinding the assembly.
“With such a diversity of bearing materials and hardness conditions, you need a full arsenal of cutting tools to profitably and efficiently manufacture them,” Giardiniere says.
The softer materials can be cut with a coated carbide, either CVD or PVD. Harder materials, such as heat-resistant superalloys, create high temperatures when cut. To maintain cutting efficiency on HRSA bearings, “we use ceramic and polycrystalline cubic boron nitride (PCBN) inserts, which can take the heat,” Giardiniere says.
For machining HRSAs, Rick Crabtree, industry specialist at Sandvik Coromant, recommends using ceramic end mills for the roughing stages because they can handle the heat, though they break down a little quicker, making the initial form less accurate. He advises switching to advanced materials such as PCBN for the insert, to cut the form of a bearing radius more accurately.
Tools and Finishing for Aerospace Bearings
In this high-heat, high-stress machining environment, special tooling techniques can preserve an insert’s accuracy for as long as possible.
“These parts are so precise that the tolerance for a ball-bearing raceway is about one-third the diameter of a hair,” Crabtree says. “The form of the race has to be almost perfectly round or it will wear on one side or the other.”
A machinist cannot straight plunge a half-inch bearing raceway with a half-inch tool, he explains, because the insert will not perform perfectly.
“We recommend using a trochoidal turning technique, starting at one edge of the race and machining all the way around with a smaller tool—maybe a quarter-inch tool to make a half-inch radius,” Crabtree says.
Edge prep on the inserts is also critical. “The PCBN is hard like an Earth diamond, but if you go in and out of a cut, you can pull its particles off,” he explains. “To prevent this, we grind a square 90-degree shoulder to start out, and then to protect the edge, we put an angle on that shoulder, making it stronger.”
Ceramic tools provide extremely high-heat cutting capabilities but need to be applied carefully because they tend to create a heat-affected zone on the workpiece, Kennametal’s Giardiniere adds.
“Part designers don’t want the surface appearance of the bearing to appear warped or marked by heat or pressure, which would show changes in the metallurgy of the base material,” he says. “Because of that, ceramics are usually reserved for roughing and semi-finishing operations, with a follow-up operation to remove any area of that surface that may have been affected by that heat.”
“For fine finishing on some applications, we’re really taking the last cut on that part,” Giardiniere says. “We may need to look at PVD-coated grades, which allow the insert tooling to have a fully sharp edge.”
“Grinding wheels are often used for the finishing processes due to the strengths of excellent surface finish and abrasive tool life, and because they can be tailored to impart a slight compressive residual stress on the ground surfaces, which helps with reducing the chances for fatigue and premature part failure,” Norton Saint-Gobain’s Biro says.
“Bearing components often will get turned in a lathe, machined or drilled,” Biro says. “Then, they’ll use super-abrasive wheels (either CBN or diamond) to grind the raceways—and the flat, parallel faces of the races—to finish dimension.”
To make bearings from start to finish, having both technologies is a good idea, he says. “They often need to work in harmony to develop the best type of product. There are areas where machining can excel, and there are areas where grinding can excel. And if you can dial in a process where you get the best of both of those things, then you’ve got a winning recipe.”
Read more: Combating Corrosion in Aerospace Parts, from Start to Finish